Composite manufacturing technologies
We combine several processes, because none of them is best for every part. We choose the process for the annual volume, the geometry, the strength and surface requirements, and the cost of moulds and machining.
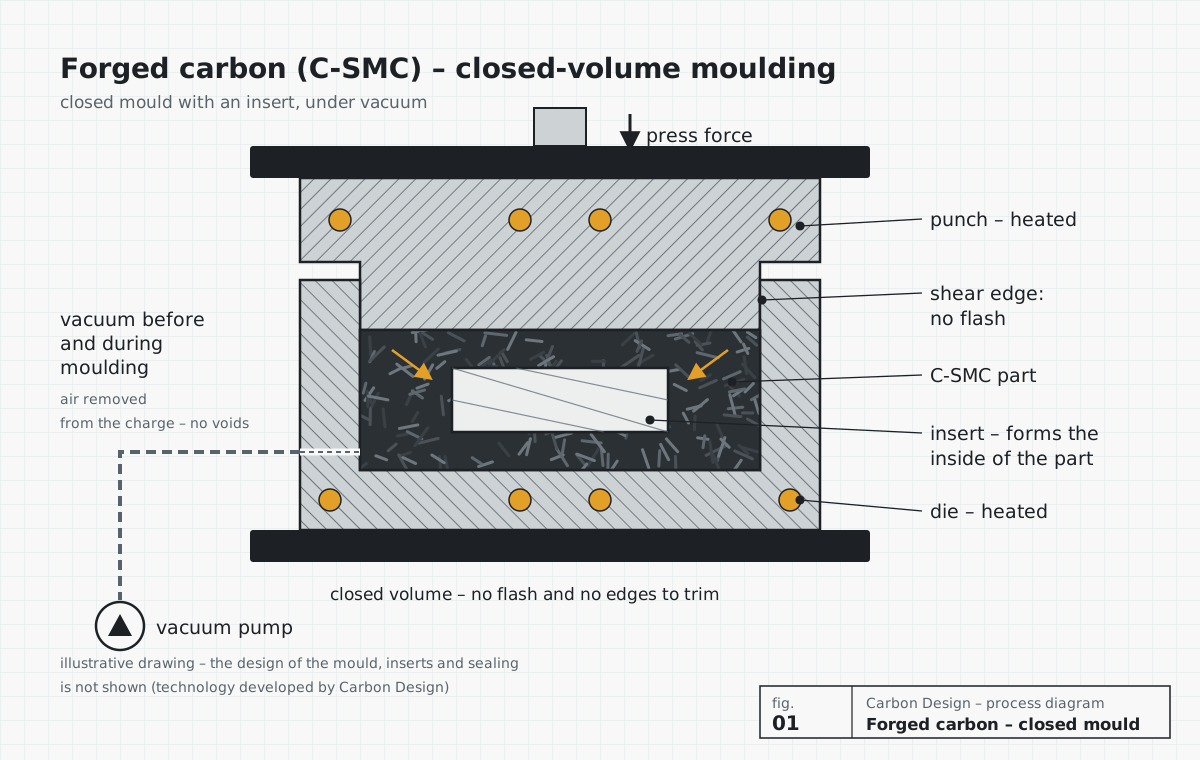
Forged carbon (C-SMC, C-BMC)
Chopped carbon fibre compression-moulded in a closed mould under vacuum – no flash and no voids. 3D parts with ribs and inserts, including hollow parts.
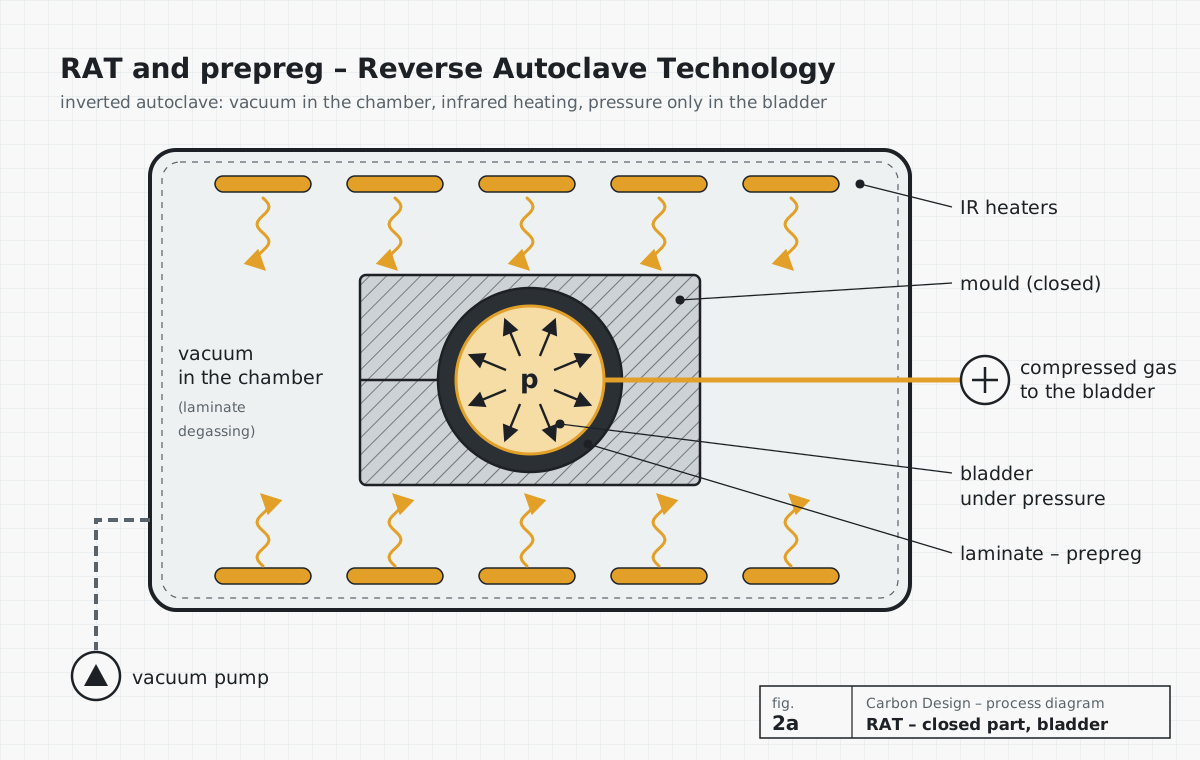
RAT and prepreg – Reverse Autoclave Technology
Hand layup of prepreg and curing under pressure. The lowest porosity and the highest properties. A more economical process than an autoclave. Inverted autoclave: the oven chamber is under vacuum, infrared heaters cure the laminate and a bag or bladder provides the pressure.
- Vacuum in the chamber
- Infrared heating
- Pressure from a bag or bladder
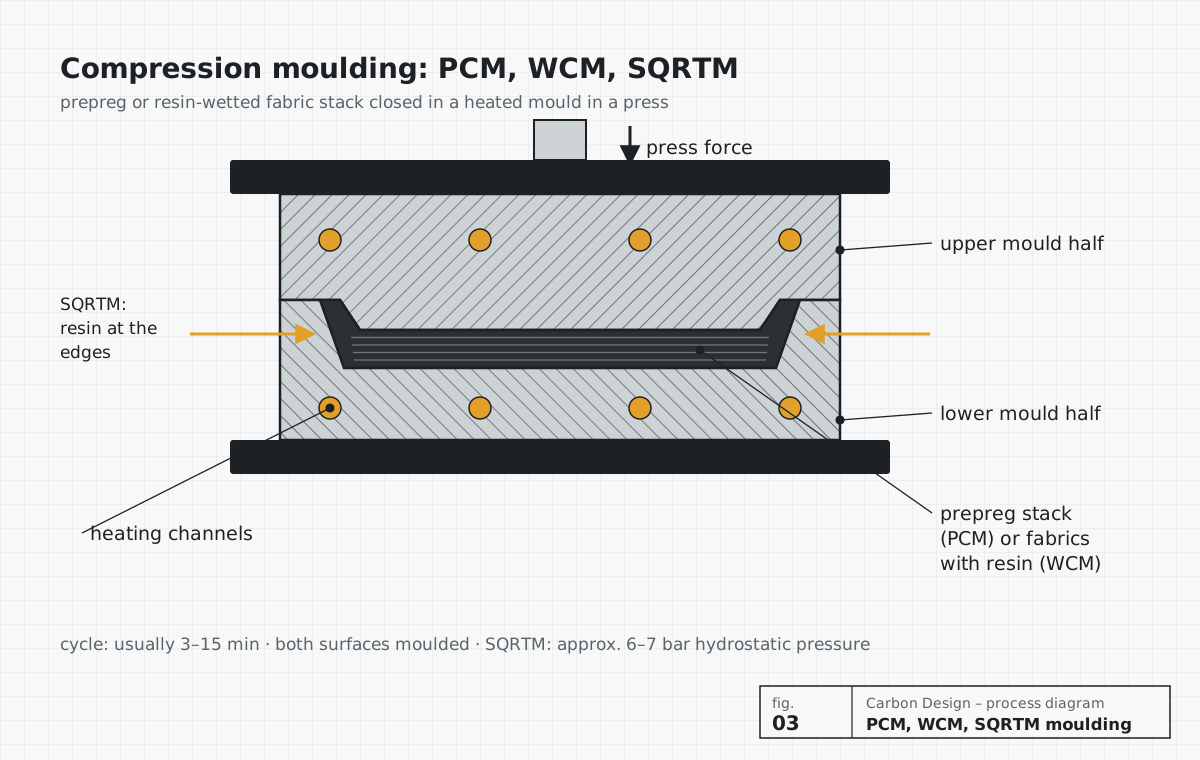
Compression moulding: PCM, WCM, SQRTM
Prepreg or dry fabrics with resin pressed in a closed mould. Both sides finished, a short cycle.
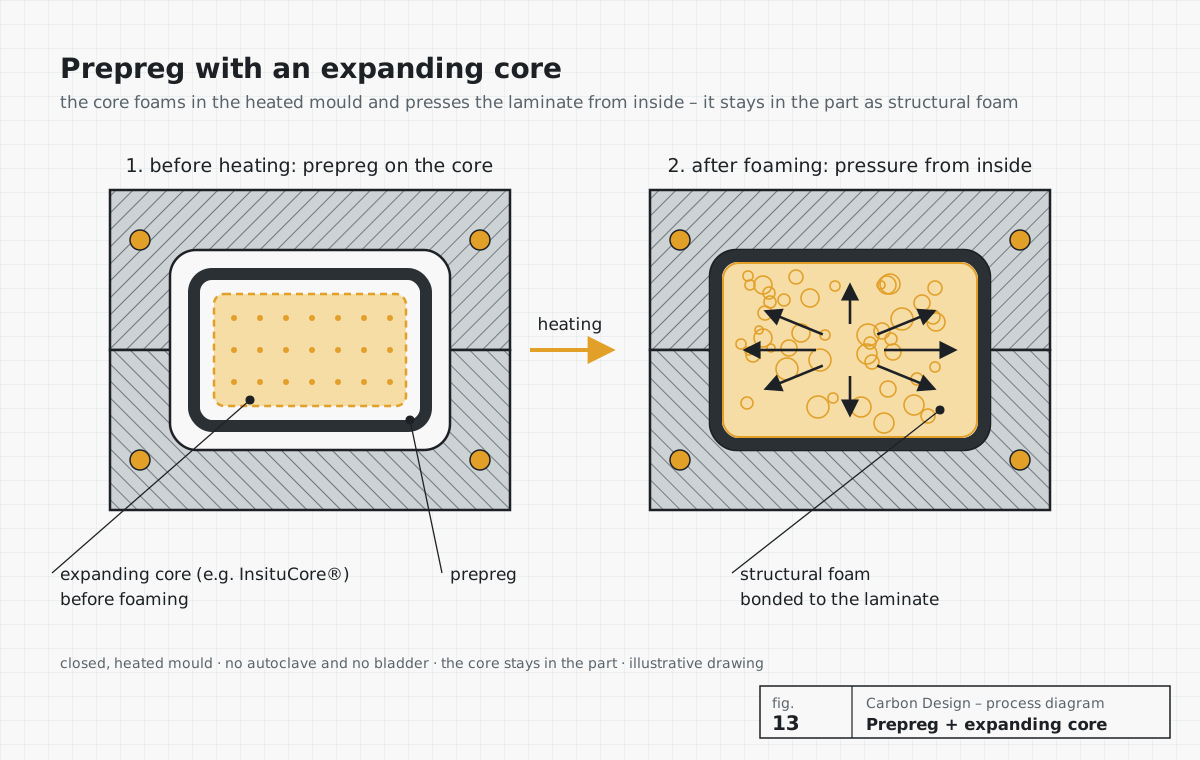
Prepreg with an expanding core
Prepreg on a core that foams in a heated, closed mould and presses the laminate from inside – e.g. InsituCore®. Profiles, frames, arms.
- Core foamed by heat
- Pressure from inside
- The core stays in the part
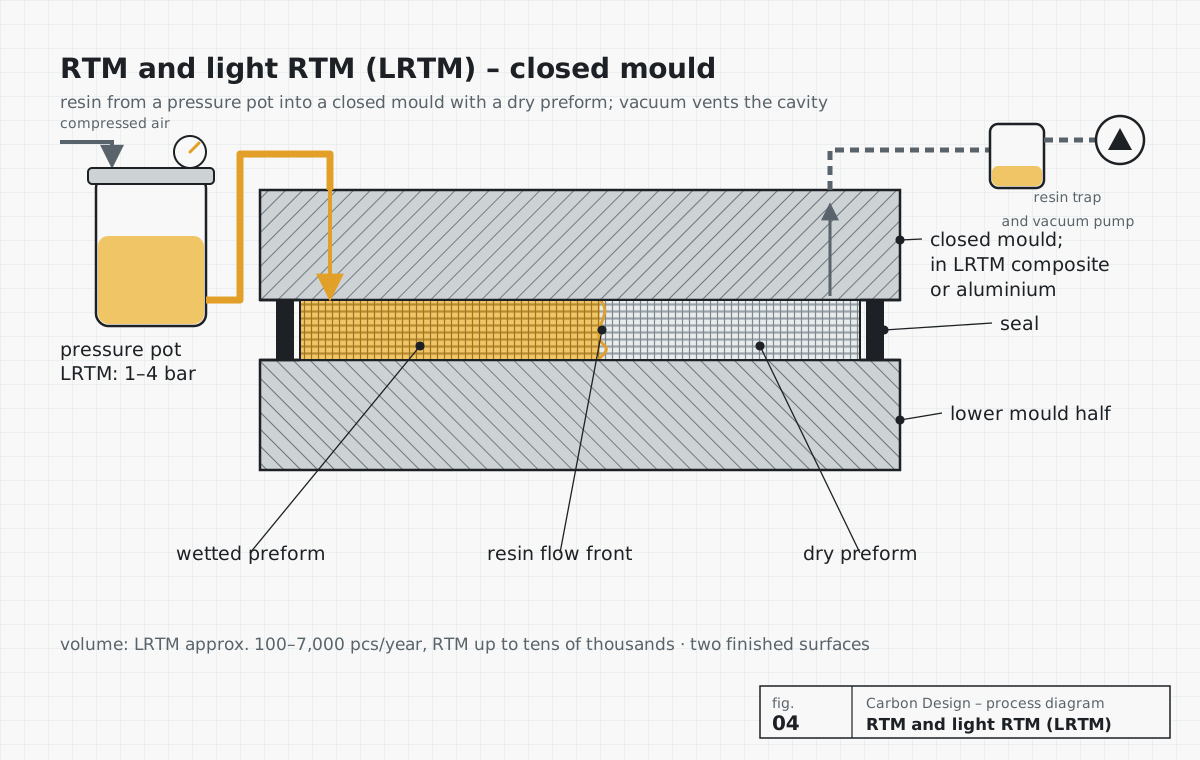
RTM and light RTM (LRTM)
Dry preforms in a closed mould, vacuum and resin injection from a pressure pot – 1–4 bar in LRTM, in composite or aluminium moulds.
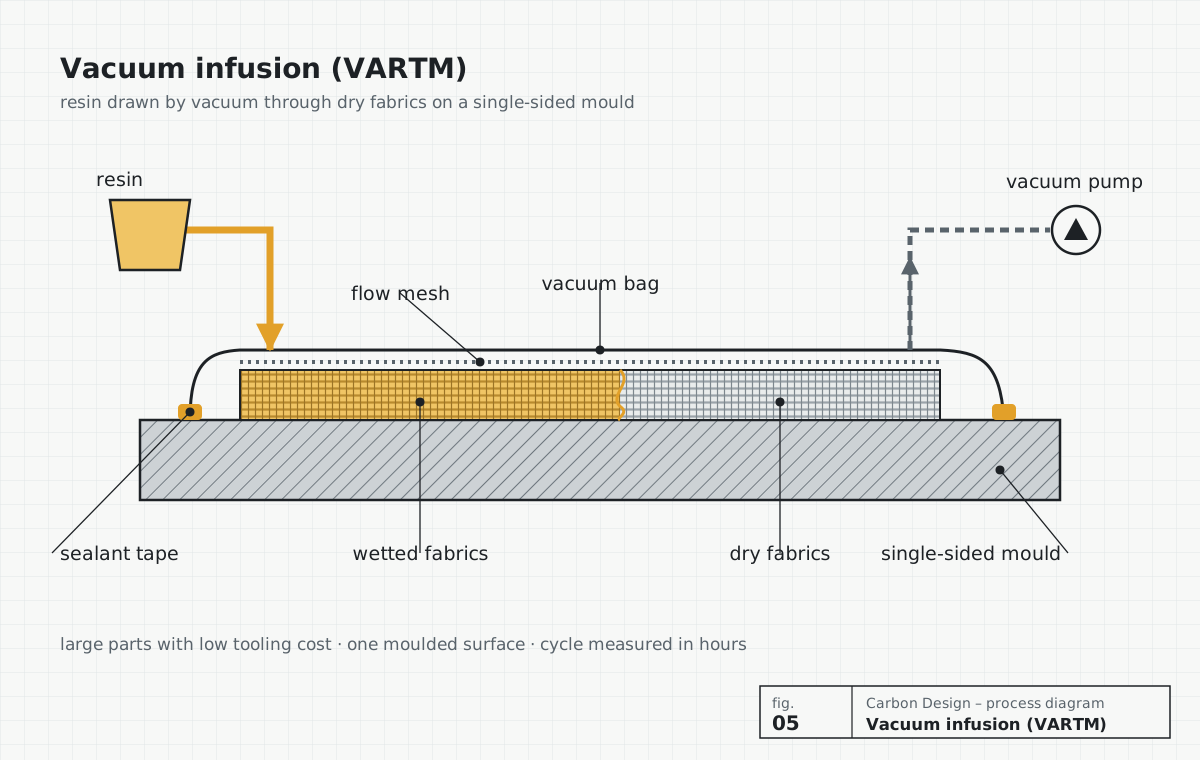
Vacuum infusion (VARTM)
Resin drawn by vacuum through fabrics on a single-sided mould. Large parts with low tooling cost.
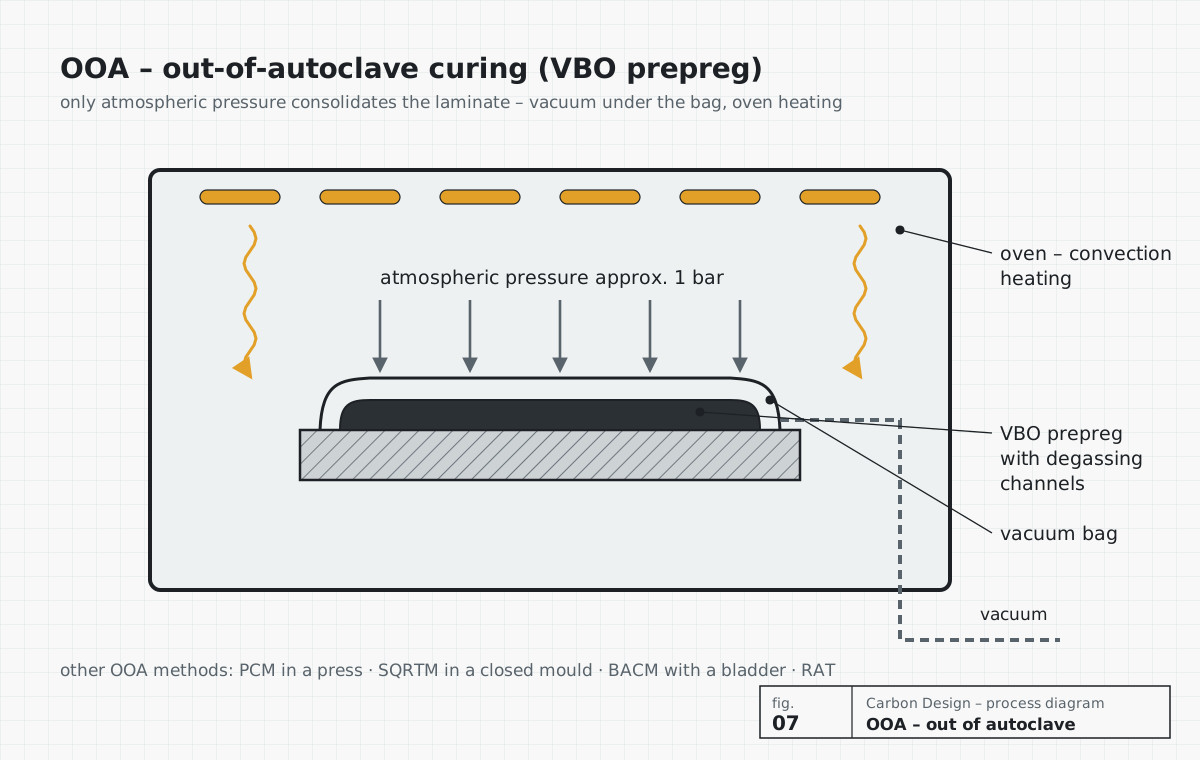
OOA – out of autoclave
VBO prepregs, compression moulding and SQRTM without an autoclave. Near-autoclave quality at a lower cost.
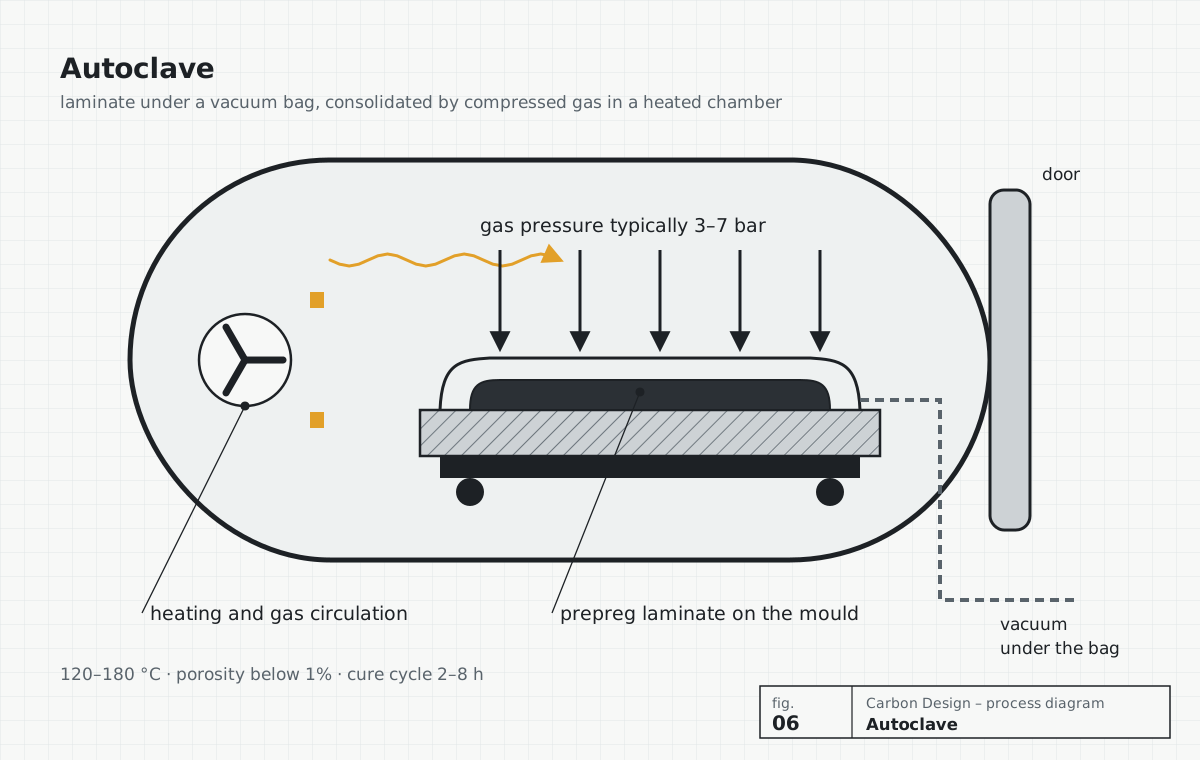
Autoclave
with partners
Hand-laid prepreg cured under pressure. The lowest porosity and the highest properties.
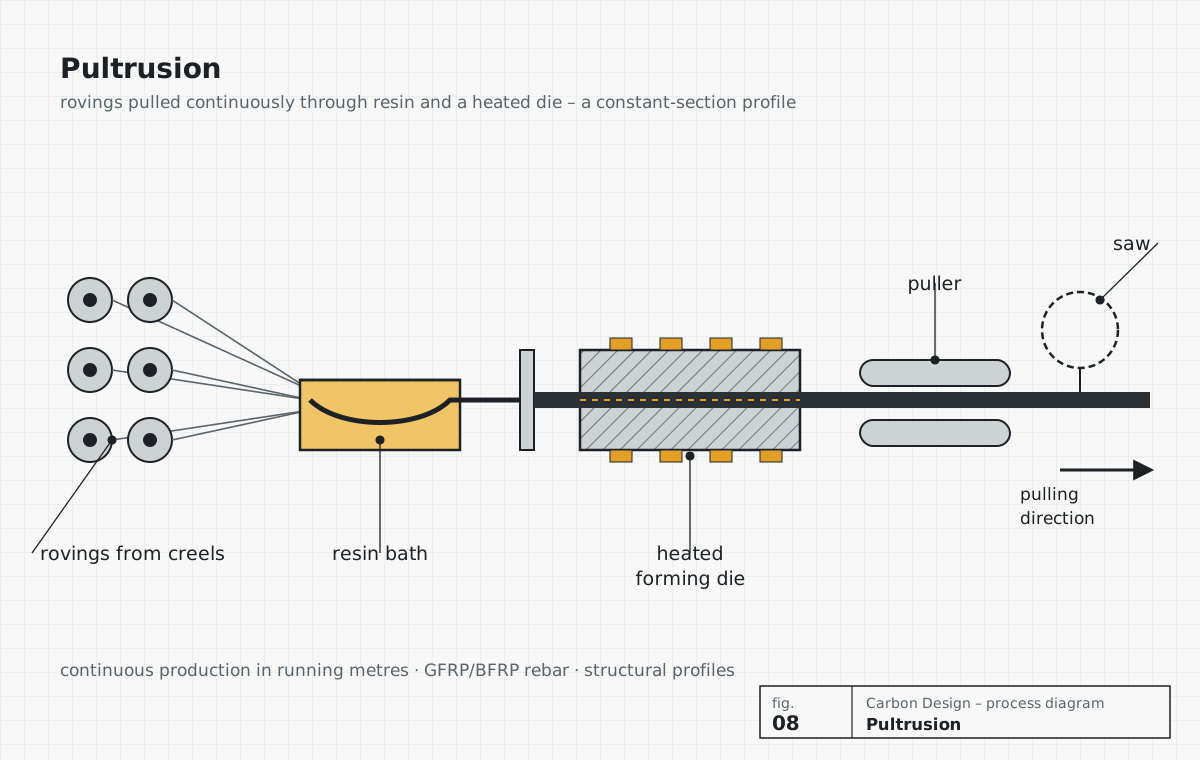
Pultrusion
with partners
Fibres pulled continuously through resin and a heated die. Rods and profiles with a constant section.
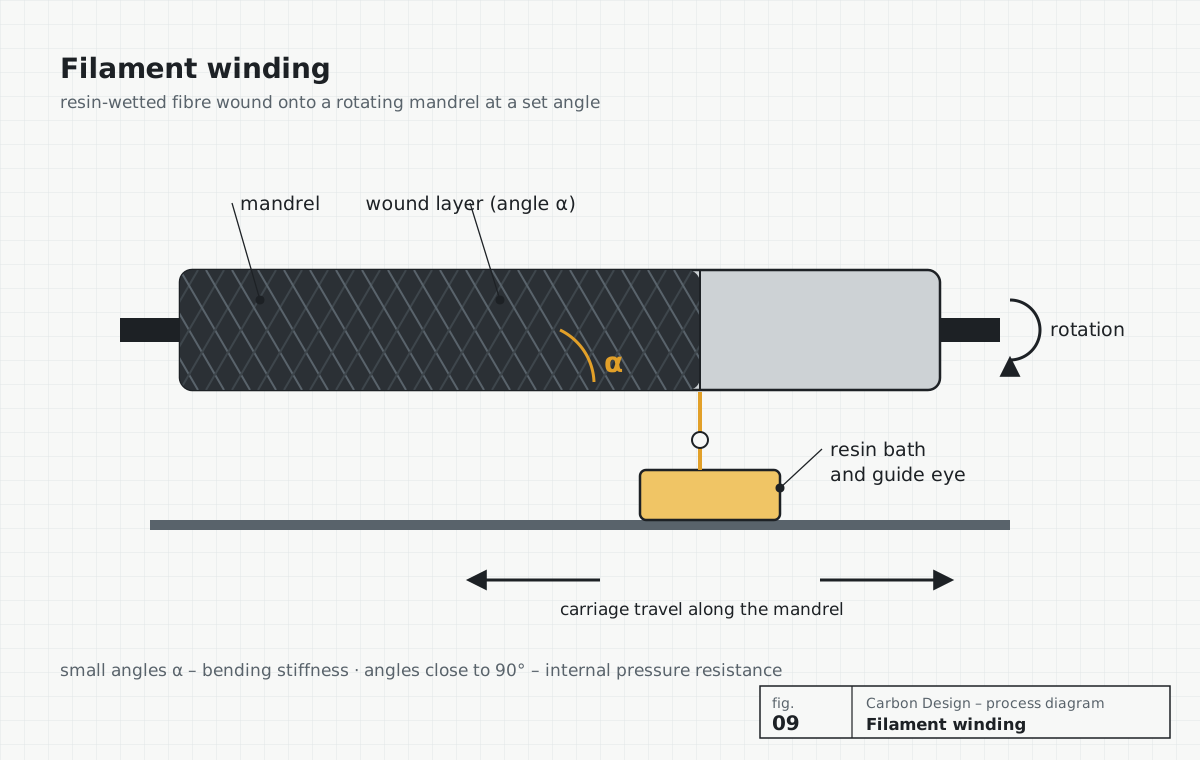
Filament winding
with partners
Fibre wound onto a rotating mandrel at a set angle. Tubes, shafts, profiles and tanks.
Process diagrams
Each process in one drawing: the mould, the material, and where the pressure and heat come from. Click a diagram to read more.
Technology comparison
One table with the key selection criteria. Volume is the typical annual quantity at which the process is usually cost-effective.
| Process | Typical volume (pcs/year) | Cycle time | Finished surfaces | Mould cost | Typical parts |
|---|---|---|---|---|---|
| Forged carbon (C-SMC, C-BMC) | 500–100,000+ | 2–30 min | 2 (closed mould) | high (steel, heated) | 3D parts with ribs and inserts, hollow parts, plates |
| RAT and prepreg – Reverse Autoclave Technology | chosen for the part | depends on the laminate | 1–2 (depending on pressure method) | depends on the pressure method | prepreg parts that need more pressure than a vacuum bag gives |
| Compression moulding: PCM, WCM, SQRTM | 1,000–50,000 | 3–15 min | 2 | high | panels, lids, covers |
| Prepreg with an expanding core | chosen for the part | depends on resin and core | 2 (closed mould) | medium (closed, heated mould) | profiles, frames, arms, sandwich parts |
| RTM and light RTM (LRTM) | 100–50,000 | 15–90 min | 2 | LRTM: low–medium (composite, aluminium); RTM: higher | housings, covers, panels, structural parts |
| Vacuum infusion (VARTM) | 1–500 | hours | 1 | low | large parts, hulls, covers |
| OOA – out of autoclave | 1–5,000 | depends on the method | 1–2 | low–high | large VBO prepreg structures, pressed parts |
| Autoclave with partners | 1–2,000 | 2–8 h cure | 1 | low–medium | aerospace structures, visible class A parts |
| Pultrusion with partners | continuous | continuous process | whole perimeter | medium (die) | rebar, profiles |
| Filament winding with partners | 50–50,000 | minutes–hours | 1 (inner) | low–medium | tubes, shafts, profiles, tanks |
How we choose the process
We start from the boundary conditions: geometry, loads, operating environment, surface requirements and planned quantity. On that basis we compare processes by the total cost of the part – not just the material.
- Annual volume and the whole production period – it decides what material the mould is made of
- Cost of moulds, machining and finishing
- Available machines and operator skills – at our plant, at yours or at a partner
- Shelf life of materials (prepregs) and the amount of waste
- Quality requirements: porosity, tolerances, surface class
Materials
| Fibre | Key properties | Typical uses |
|---|---|---|
| Carbon fibre (CFRP) | the highest stiffness and strength at low mass | structures, visible parts, motorsport, aviation |
| Glass fibre (GFRP) | good strength, low cost, electrical insulation | covers, housings, rebar |
| Aramid (Kevlar) | impact and cut resistance | ballistic and protective covers, impact zones |
| Basalt fibre | chemical and thermal resistance | concrete reinforcement, heat shields |
| Natural fibres | lower carbon footprint | interior parts, non-structural parts |
Resins: epoxy, bio-based and vinyl ester. We also use resin casting and automated tape laying (ATL) when the part calls for it.
Questions and answers
How do I choose a manufacturing process for a composite part?
The annual quantity, the geometry and the requirements matter most. Prototypes and small series usually use autoclave prepreg, RAT, OOA or infusion; medium series light RTM or compression moulding; large series forged carbon (C-SMC), PCM or RTM. We confirm the choice with a total cost analysis.
Which composite process is the cheapest?
There is no single answer: the smaller the series, the more the mould cost matters; the larger it is, the more the cycle and material cost matter. Infusion has cheap moulds but a long cycle; forged carbon has expensive moulds but a cycle measured in minutes.
What is the difference between autoclave, RAT and OOA?
In an autoclave compressed gas fills the chamber and presses the laminate. In RAT the chamber is under vacuum, infrared heaters provide the heat and a pressurised bag or bladder provides the pressure. In OOA the laminate cures without an autoclave: under a vacuum bag in an oven, in a press or in a closed mould.
Can you set up a process at our plant?
Yes. We design the moulds and the process, start up production at your facility, train the operators and hand over the process documentation.
External data sources: Wikipedia – Out of autoclave composite manufacturing.
Have a drawing or just an idea? We will tell you how to make it.
Tell us what the part has to do, how many you need and what the requirements are. We will reply with a proposed process, material and next steps – with no obligation, under NDA if needed.